Dispensing & Sampling Booths
- Home
- Dispensing & Sampling Booths
Dispensing & Sampling Booths provide protection from airborne contaminants generated during powder handling operations such as sampling, charging and dispensing.
Note that a Reverse Laminar Air Flow Unit provides:
The downflow booth operates on a recirculatory airflow principle providing containment by air movement. Within the work area, a clean, constant, laminar downflow of Class 100 air is supplied to suppress any dust clouds generated during open powder processing, removing and capturing airborne particles from the operator’s breathing zone.
Ensure operator, product, and environmental protection with high-performance RLAF booths. Designed for safe powder handling, these systems control airborne contaminants through efficient filtration and uniform laminar airflow. Their recirculatory design minimizes dust dispersion and enhances workplace safety during pharmaceutical powder-processing operations.
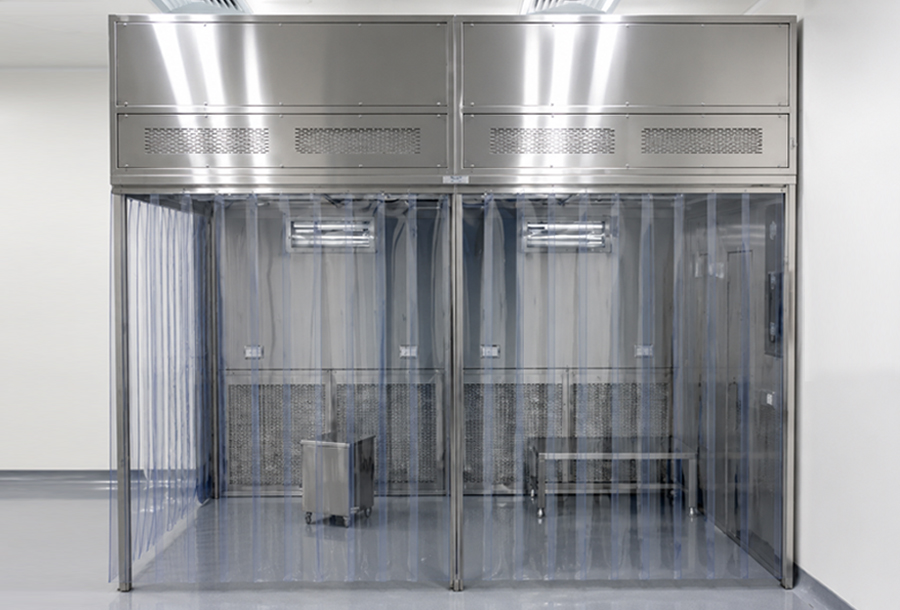
The prefilters at the base of the rear wall capture the airborne contaminants. The intake velocity at prefilters increases to ensure scavenging effect.
A small percentage of air is discharged from the booth through the bleed exhaust HEPA filter to maintain the working space under negative pressure. RLAF is available in GI powder coated / SS304 / SS316 or combination.